


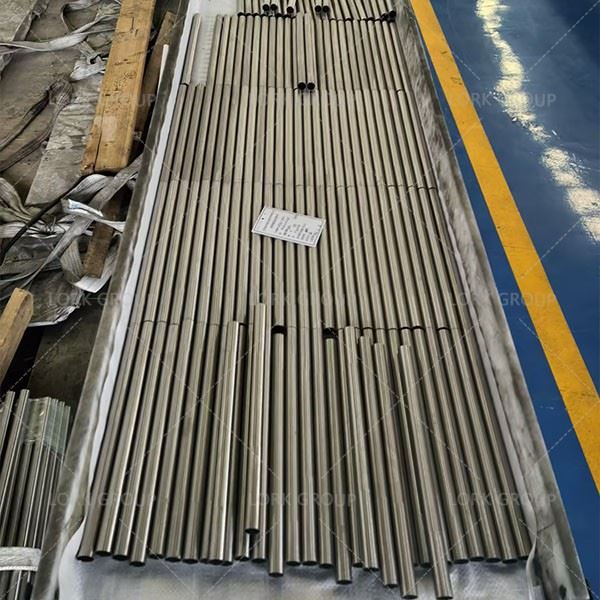


HyMu 80 Permalloy Alloy Tube
Product Introduction
HyMu 80 is a permalloy with magnetic permeability. Its core characteristics are extremely high initial permeability, extremely low coercivity, and the addition of molybdenum (Mo), a key additive. In short, it is an electromagnetic functional material that "efficiently conducts magnetism in weak magnetic fields, leaves no residual magnetism after the magnetic field is removed, and has low loss at high frequencies." Our customers purchase it for use in precision transformers, magnetic shielding bushings, or electromagnetic components requiring weak signal transmission.
It is worth noting that precision electromagnetic components have high requirements for surface cleanliness. Oil stains and rust will affect subsequent processing. When we were manufacturing Permalloy pipes for a customer, the surface of the pipes was accidentally exposed to moisture due to a week of heavy rain while being stored in the warehouse, causing localized rust. As a result, we had to urgently produce another batch of pipes for the customer. In addition, the inner and outer surfaces of Permalloy pipes must not have cracks, folds, scratches, or oxide scale.
Industry Standards and Procurement Specifications
When customers inquire about HyMu 80 tubes, unlike bars and strips, the most difficult aspect of manufacturing is controlling the precision of parameters such as wall thickness, inner and outer diameters, and length. This puts a great strain on the supplier's manufacturing capabilities.
1. Standards Applied:
ASTM A753: This is the core standard for nickel-iron soft magnetic alloys. HyMu 80 corresponds to the Alloy 8 type.
GB/T 15018: Domestic standard, corresponding to grade 1J85 (similar composition and properties).
Customer Drawings: Often, these precision materials are manufactured according to the technical agreements provided by the customer's drawings; standards are only for reference.
2. Dimensions (Specific to Alloy Tubes):
Outer Diameter (OD) x Wall Thickness (WT): Common Permalloy alloy tubes range from an outer diameter of 6-100mm and a wall thickness of 0.5-10mm. It's important to specify whether it's a cold-drawn seamless tube or a welded tube. Precision electromagnetic components generally require cold-drawn seamless tubes due to their high dimensional accuracy and smooth inner wall.
Length: Typically 2-6 meters, but custom lengths are also available. If used for magnetic shielding sleeves, length tolerances may need to be specified.
Straightness: Slender tubes require high straightness; the allowable bend per meter (in millimeters) must be specified.
Special reminder: The delivery condition of Permalloy tubes is extremely important! We provide two delivery conditions based on customer requirements: annealed and cold-drawn. So how do you choose?
If you're buying them to directly assemble into components (then annealing is required), or if you're buying them to process and then anneal them yourself (cold-drawn is acceptable)?
Processing difficulty and key points
(This is the key to saving money)
HyMu 80 has similar processing properties to austenitic stainless steel (such as 304), and the following points should be noted during processing.
Heat Treatment (This is the lifeblood of HyMu 80):
- Intermediate Annealing (Softening during processing):
Must be protected with dissociated ammonia, hydrogen, vacuum, or inert gas. These high-nickel alloys readily absorb carbon, sulfur, and oxygen from the furnace atmosphere, causing a sharp drop in magnetic properties after contamination. Temperature should be controlled at 788-1010°C, and the time should not exceed 1 hour.
- Final Annealing (For optimal magnetic properties):
Must be done with dry, pure hydrogen with a dew point <-40°C. This is the standard process; vacuum annealing will result in slightly inferior performance. The temperature needs to be controlled at 1121-1177°C, and the time at 2-4 hours. Simultaneously, the furnace should be cooled to 593°C, and then cooled at a controlled rate of 194-334°C/hour between 593°C and 371°C.
Regarding final cleanliness: Before annealing, all oil, paint, and contaminants must be thoroughly removed. The parts should be separated by magnesium oxide and aluminum oxide powder to prevent them from sticking together.
For more information, please contact:
Email: susan@lorkgroup.com
WhatsApp: +86 19937075488

Chemical Composition
Special reminder: The chemical composition of HyMu 80 alloy must contain extremely low levels of impurities such as carbon (C), sulfur (S), and phosphorus (P), with strict control over trace values. For example, in the supplier's melting report, the lower these numbers are, the higher the level of vacuum melting and the more stable the magnetic properties.
| Weight% | Permalloy Alloy |
| Ni | 79.0-81.0% |
| Mo | 3.8-5.2% (Key Additives) |
| Fe | 14-16% |
| Mn | ≤1.1% |
| C / S/ P | trace amounts |
Mechanical Properties
(Annealed state, typical value)
| Material | Reference value |
| Tensile Strength | ≥690 MPa (100,000 psi) |
| Yield Strength (0.2%) | ≥300 MPa (44,000 psi) |
| Elongation | ≥40% |
| Hardness | ≤80 HRB |
Physics and magnetic properties (this is the core)
| Performance Specification | Typical Values |
| Initial permeability (μi) | 20,000 - 50,000 |
| Maximum Permeability (μm) | 100,000 - 200,000 |
| Coercivity (Hc) | < 2 A/m |
| Saturation Magnetic Induction (Bs) Approx | 0.75 - 0.8 T |
| Resistivity (ρ) | 55-62 μΩ·cm |
Special Reminder: Based on our experience with HyMu 80 alloy orders, magnetic properties are the core of acceptance testing, not mechanical properties. Suppliers must provide a measured magnetic property report, specifically measured according to ASTM A596/A773 standards.
Key Points of Quality Inspection Process
Acceptance criteria are the core of qualified delivery.
-
Dimensional Tolerances:
Initial and secondary inspections of HyMu 80 alloy tubes are conducted using a micrometer to randomly sample and check multiple points to ensure compliance with ASTM B751 or drawing tolerances.
Straightness: Slender tubes are placed on a platform and measured using a feeler gauge.
-
Magnetic Performance Testing: For these materials, we will explain to the customer that we will conduct magnetic performance testing before shipment. This is generally done according to ASTM A596 or A773 standards, measuring DC magnetic properties and issuing a data report including initial permeability (μi), maximum permeability (μm), coercivity (Hc), and saturation magnetic induction (Bs).
When reviewing this report, if the data do not match, for example, μi < 20,000, Hc > 2 A/m, it is highly likely that the annealing treatment was substandard. In this case, the material needs to be returned or re-annealed.
- Chemical Composition Report: Taking the chemical composition of Permalloy alloy tubes as an example, using a handheld spectrometer to test the composition, the following should be checked: Nickel (Ni) content should be between 79-81%; below 78%, the magnetic permeability will not be high enough. Molybdenum (Mo) content should be between 3.8-5.2%; a deficiency will result in poor high-frequency performance. The report also includes the content of other elements such as carbon (C) and iron (Fe).
For tests such as surface quality, mechanical properties, and non-destructive testing, we will conduct the tests we require after consultation.
Hot Tags: hymu 80, permalloy alloy,alloy tube, China hymu 80 permalloy alloy tube manufacturers, factory
You Might Also Like


Send Inquiry